








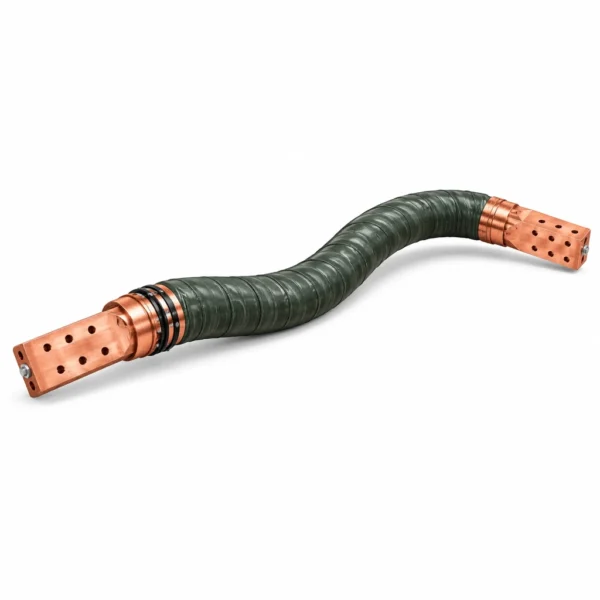
EAF Water Cooled Cable
EAF water cooled cable is a flexible copper connection for electric arc furnace secondary circuits: 5500 mm² total copper section, 11 m overall assembly length, circulating water cooling and a swivelling terminal at one end.
Specified water working pressure: 4 bar. Hydraulic test requirement: 6 bar. Terminal interfaces follow the approved project drawing.
Product illustration. Final construction and terminal details follow the approved project specification.
EAF water-cooled cable for furnace secondary circuits
The TEBAOFLEX EAF water-cooled cable is a flexible copper connection for the secondary circuit of an electric arc furnace. This configuration has a nominal total copper cross-section of 5500 mm² and an overall assembly length of 11 m, including both terminal extensions. Circulating water provides cooling through the assembly, while one end incorporates a swivelling terminal.
For a furnace maintenance team, the purchasing task is to match the complete assembly to the installation. The flexible conductor, cooling circuit and end connections must work together within the available routing space. The specified bend radius and cable body envelope provide useful starting points when reviewing that space.
For a replacement or new installation, compare the terminal contact arrangement, mounting orientation, cooling-water connections and installed cable route against the approved project drawing. Copper section and overall length identify the requested configuration; the interface review establishes how it connects to the furnace secondary system.
The technical tabs below bring the construction, application and dimensional requirements together for procurement review. Water working pressure and hydraulic test pressure are listed separately so the operating requirement and inspection requirement remain clear. Share the installation requirements with TEBAOFLEX when requesting a quotation so the assembly details and inspection scope can be agreed before manufacture.
For related cable types, explore the Industrial Cables range.
For related steelworks melt-shop reeling cables and flexible secondary welding leads, compare these specifications: Ladle Transfer Car & Steel Mill High-Temperature Reeling Cable (0.6/1 kV) (for motorized hot-metal ladle transfer car reeling drums at 0.6/1 kV); WCT Welding Cable for Arc Welder Secondary Leads (for air-cooled flexible copper secondary welding leads). Verify nominal cross-section up to 6000 mm², cooling-water pressure, and copper terminal lug dimensions before ordering.
For complete multi-model sizing across 750 mm² to 7,000 mm² furnace secondary circuits and meltshop reeling feeders, compare: High-Current Water-Cooled Furnace Cable Series (1,000–7,000 mm² OC25–OC70 & 30510–30534) (covering 5–25 kA flute-core, perforated-LSOH multi-rope, and 750–1,500 mm² S.A.F. ring-nut models); Ladle Transfer Car & Meltshop High-Temperature Reeling Cable (for mobile ladle car and hot-metal crane reeling service). Match rope cross-section, terminal type (Types 1–9), and cooling hose temperature class to your furnace installation.
Flexible copper assembly with one swivelling end
The EAF water-cooled cable uses flexible copper ropes and copper end terminals. A cooling-hose assembly contains the conductor and circulating cooling water. The terminal arrangement has a swivelling device at one end and a fixed connection at the opposite end.
- Conductor: flexible copper ropes, with 5500 mm² total nominal copper section per assembly.
- End connections: copper terminals matched to the approved project interface.
- Cooling: circulating water through the cable assembly.
- Terminal movement: one swivelling end; opposite end fixed.
Confirm the hose, seals, insulation and fixing details during the project review. The final assembly must fit the specified cable body envelope and connection arrangement.
Electric arc furnace secondary-circuit connections
This configuration is intended for a flexible, water-cooled high-current connection in an EAF secondary circuit. It is relevant to steelworks maintenance buyers, furnace equipment suppliers and project engineers reviewing a replacement assembly or a new furnace connection.

Before selecting the assembly, review the installed route, available space, terminal orientation and cooling circuit. Confirm that the route accommodates the specified minimum bend radius and body diameter throughout the required furnace movement.
Provide the operating current, AC or DC duty, operating frequency and cooling-water conditions for engineering review. These inputs are required to assess the connection in its actual furnace circuit and to agree the final assembly specification.
For electric arc furnace delta closures, ladle refining furnaces, and secondary high-current leads, review these options: Welding Cable Supplier for Custom Flexible Leads & Bulk Cable (for custom air-cooled flexible welding leads and bulk secondary power cables); H01N2-D / H01N2-E Welding Cable 100/100 V (for harmonized rubber-sheathed manual and automated arc welding leads at 100/100 V). Confirm furnace swing geometry, cooling flow rate, and terminal bolt pattern before fabrication.
EAF water-cooled cable: specified configuration
| Parameter | Specified value |
|---|---|
| Application | Electric arc furnace secondary circuit |
| Nominal conductor cross-section | 5500 mm² total copper section per assembly |
| Overall assembly length | 11,000 mm (11 m), including both terminal extensions |
| Cable body reference length | 10,360 mm, between terminal reference planes |
| Conductor and terminal material | Copper |
| Maximum cable body diameter | 253 mm |
| Minimum bending radius | 1000 mm |
| Terminal arrangement | One swivelling end; opposite end fixed |
| Cooling method | Circulating water |
| Specified water working pressure | 4 bar (0.4 MPa) |
| Hydraulic test requirement | 6 bar (0.6 MPa) |
| Terminal interface | As specified in the approved project drawing |
Agree operating current, electrical duty, cooling-water flow and temperature conditions during the quotation review. Terminal geometry and cooling-water connections are confirmed against the installation interface.
Project specification and inspection requirements
The specification basis for this EAF water-cooled cable is the approved project drawing and the agreed assembly requirements. Use the following points when establishing the order inspection scope.
| Review item | Project requirement |
|---|---|
| Conductor configuration | 5500 mm² nominal total copper section per assembly |
| Dimensional review | 11 m overall length, 253 mm maximum cable body diameter and 1000 mm minimum bending radius |
| Terminal interface review | Match the approved connection drawing and single-end swivelling arrangement |
| Water circuit operating requirement | 4 bar (0.4 MPa) specified working pressure |
| Hydraulic inspection requirement | 6 bar (0.6 MPa) test pressure; test procedure, duration and acceptance criteria to be agreed in the project inspection plan |
Specify the required inspection records and order documentation during the quotation review.
Related cable options
Compare these cable options by service combination, movement, load, voltage and transmission requirement.
WCT Welding Cable for Arc Welder Secondary Leads
A related cable option for a different application or duty profile.
View product
H01N2-D / H01N2-E Welding Cable 100/100 V
A related cable option for a different application or duty profile.
View product
Ladle Transfer Car & Steel Mill High-Temperature Reeling Cable (0.6/1 kV)
A related cable option for a different application or duty profile.
View productRequest a cable recommendation and quotation
Send the required services, cable length, mechanical duty, environment, termination and quantity. Our team will review the application before quoting.
- Include the product name or SKU plus the required cable length and quantity.
- Attach a specification, drawing or data sheet when available.