
Mobile equipment cable durability
On mobile mining equipment, the jacket is almost always the first thing to fail, long before the conductor, insulation or screen give any trouble. Drag over rib and floor, crushing under tyres and tracks, repeated contact against a reel or roller — the outer sheath wears through while everything electrical inside it is still fine. Picking an abrasion resistant mining cable for mobile equipment means matching jacket and construction to how the machine actually moves the cable.
Abrasion-resistant mining cable at a glance
- Abrasion resistance
- The jacket’s ability to resist material loss from repeated rubbing against rock, steel, concrete or a reel surface. Compound, wall thickness and construction all contribute; the compound name on its own tells you very little.
- Where it matters most
- Mobile equipment — trailing cables dragged over rib and floor, reeling cables wound and unwound under tension, and anything running through guides, sheaves or rollers.
- How it is tested
- Rotating-drum abrasion tests such as ISO 4649 or DIN 53516 measure volume loss when a sample is rubbed against a standard abrasive sheet. Lower volume loss means better resistance.
- Common jacket families
- CPE (chlorinated polyethylene), TPU/PUR (thermoplastic polyurethane) and PVC. Each trades abrasion performance against cost, flexibility, flame behaviour and cold-temperature service.
- What it is not
- You can’t compare a number across manufacturers without knowing the test method and sample thickness behind it, and a good jacket doesn’t fix a badly routed cable — it just fails a bit later.
Why the jacket fails before anything else on mobile equipment
A mining cable carries current through a conductor, keeps it isolated with insulation and, on shielded constructions, grounds fault current through a screen. None of that has anything to do with abrasion. The jacket is the only layer between all of it and the route surface, and on mobile equipment that surface rarely does the cable any favours.
Cable dragged behind a continuous miner, shuttle car or LHD crosses rib, floor and steel crossings repeatedly during a shift. Reeling cable on a crane, drill jumbo or reclaimer takes sustained contact against the drum, level-wind mechanism and guide rollers every time it pays in or out. Once the jacket wears through, moisture, dust and fines reach the bedding and the screen, and what started as a cosmetic wear mark becomes an insulation or grounding fault.
Crushing is a separate mechanism. A cable left on the floor and driven over by a shuttle car, LHD or supply vehicle gets crushed, not abraded. Repeated crushing flattens the conductor and work-hardens the strands before the jacket ever shows visible damage, and a compound built to resist abrasion won’t necessarily resist crushing, or the other way round.
How abrasion resistance is measured
Jacket abrasion is normally reported against a rotating-drum abrasion test — ISO 4649 internationally, or the closely related DIN 53516 method common on European datasheets. Both rub a test piece against a standard abrasive sheet on a rotating drum and report the material lost as a volume, so a lower number means the compound resists wear better.
| What it does tell you | What it does not tell you |
|---|---|
| Relative wear rate of one compound against a standard abrasive under lab conditions | How the jacket behaves against site-specific abrasives such as sharp rock, weld spatter or concrete dust |
| A repeatable number for comparing compounds tested to the same method and thickness | Performance against crushing, impact cuts or chemical attack — those are separate test methods |
| Whether one supplier’s own material improved between formulations | A direct comparison across suppliers unless the test method, sample thickness and conditioning all match |
A datasheet that quotes an abrasion figure without naming the test method is giving you a marketing number, not an engineering one. Ask for the method and the sample preparation before using it to compare two constructions.
CPE, TPU/PUR and PVC compared for abrasion duty
Most mobile mining equipment cable uses one of three jacket families: chlorinated polyethylene (CPE), thermoplastic polyurethane (TPU, usually labelled PUR on European datasheets), or PVC. Swapping one for another changes more than abrasion resistance. Oil is the other axis these same three compounds are ranked on, and the order is not the same one — how the PR I and PR II oil ratings compare covers that trade where a route is oiled as well as abrasive.
| Property | CPE (thermoset) | TPU / PUR (thermoplastic) | PVC |
|---|---|---|---|
| Relative abrasion resistance | Good — the long-standing mining default | Very good to excellent; one published manufacturer comparison reports its TPU jacket losing roughly a fifth as much material as its own CPE jacket in the same drum test | Moderate — suited to lighter or protected duty |
| Tear and cut resistance | Good | Better than CPE in most published comparisons | Lower |
| Processing | Cross-linked (vulcanised) after extrusion — an extra manufacturing step | Extruded thermoplastic, no cross-linking step | Extruded thermoplastic |
| Cold flexibility | Good down to typical mine ambient ranges | Generally good; confirm the specific grade’s low-temperature rating | Stiffens noticeably in cold conditions |
| Flame and smoke | Halogenated; can produce more smoke in a fire | Halogen-free grades available; confirm per grade | Halogenated |
| Typical mobile-equipment role | Heavy trailing power cable, established mine practice | Reeling cable, compact control cable, outdoor mobile power where abrasion and UV both apply | Light control, signal or short compact-reel duty |
That TPU-versus-CPE comparison is one manufacturer’s own third-party test data for its specific formulations. A different CPE or TPU grade won’t necessarily repeat the same ratio, so use it as evidence the effect is real rather than a number to copy into a specification.
Construction factors beyond the compound
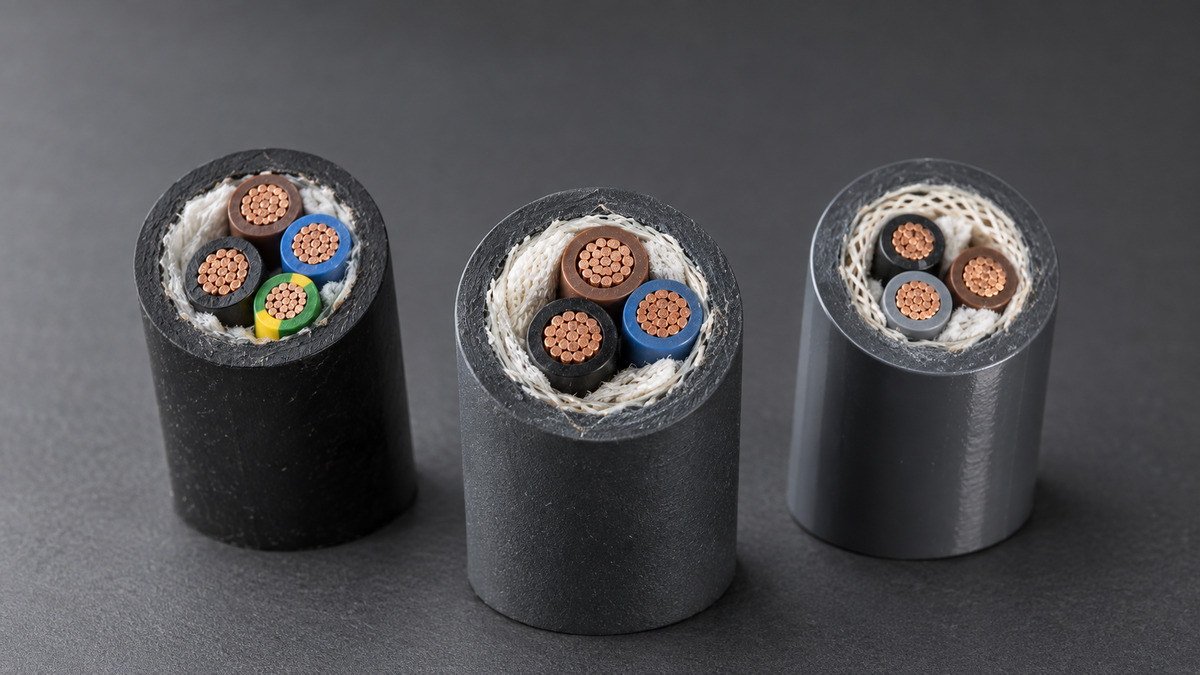
Two cables can share the same jacket compound and still wear at very different rates, because construction sets the rest of the outcome.
- Wall thickness — more material means more to wear through before the bedding is exposed, independent of how fast the compound itself wears. It also adds stiffness and weight, which works against flex life on a trailing route.
- Reinforcement braid. A textile or wire braid under the jacket won’t stop the wear itself, but it slows moisture ingress once the outer layer opens up and holds the construction together in the meantime.
- Bedding and separator layers under the jacket keep the screen and cores protected for a while even after visible wear starts, buying time between inspection and a forced replacement.
- Round versus flat profile. Flat cable spreads contact over a wider bearing surface on some routes and can even out wear — that’s a route call, though, not a blanket abrasion upgrade.
A material name by itself, without wall thickness and construction specified, doesn’t tell you much. Ask for both when comparing datasheets.
Match the jacket to the movement duty, not just the machine
What wears the jacket is how the cable moves, not which machine it’s bolted to — a trailing cable and a reeling cable wear against completely different surfaces, so the jacket priority shifts with the duty.
| Duty | Primary wear mechanism | Typical equipment | Jacket priority |
|---|---|---|---|
| Trailing, dragged | Sustained drag over rib, floor and crossings; risk of crushing where equipment runs over slack cable | Continuous miners, shuttle cars, LHDs, drills | High abrasion and cut resistance, adequate wall thickness for the drag distance |
| Reeling, powered or spring | Repeated contact with the drum, level-wind mechanism and guide rollers under tension | Cranes, drill jumbos, reclaimers, dredges | Abrasion resistance plus a construction rated for the specific reel’s bend radius and tension |
| Guided or festooned | Contact with trolleys, guides and support points along a fixed path | Gantries, conveyor tripper cars, some drill rigs | Abrasion resistance at defined contact points more than along the full length |
| Compact spring reel, light duty | Lower cycle counts, protected entry point, limited random winding | Portable control panels, small service reels | Moderate abrasion resistance is often adequate if entry protection (mesh grip, shock absorber) is used |
See reeling cable versus trailing cable for how to decide the movement duty itself before specifying the jacket, and the eight-step mining cable selection guide for the full specification sequence this sits inside.
How the ore body and the jurisdiction change the answer
TEBAOFLEX supplies mining and heavy mobile equipment cable into more than 20 countries, and the enquiries fall into a handful of recognisable patterns. Movement duty sets the wear mechanism, as above. The site conditions and the governing jurisdiction then decide which construction family that duty gets built in.
| Region and operation | What dominates jacket exposure | Construction family usually specified |
|---|---|---|
| Central African copper–cobalt belt (DR Congo, Zambia), plus coal | Wet, abrasive haul and tailings routes; long drag distances between reposition points | IEC and DIN VDE designations — the (N)SHÖU and (N)TSCGEWÖU rubber families |
| South American copper and iron ore (Chile, Peru, Brazil, Argentina) | Strong UV and dry abrasive dust, often at altitude, with long surface drag runs | PUR-sheathed constructions, where UV and abrasion have to be answered together |
| South-East Asian nickel and coal (Indonesia, Malaysia, Vietnam) | Wet laterite mud, sustained heat and humidity, heavy mobile plant crossing cable routes | Rubber trailing and reeling constructions; crush protection weighs as heavily as wear rate |
| Australia (coal and metalliferous) | Mixed conditions, but the standard is usually settled before the site conditions are discussed | AS/NZS 1802 and 2802 — the Type 209, 240, 241 and 275 families |
| China (coal) | Underground mobile face equipment under national mine-safety rules | MT/T 818 series: MYP, MYPT and MYPTJ shielded rubber constructions |
| North America | Portable power to continuous miners, loaders, drills and shovels | Built to ICEA S-75-381 — SHD-GC, Type W and Type G-GC; the MSHA acceptance route is confirmed per project |
Two things follow. First, the same abrasion duty gets solved four or five different ways depending on which standard family the site works to, which is why our mining range carries parallel constructions rather than one flagship cable. A Chilean open-pit drag route and an Australian underground coal route can face comparable wear and still arrive at completely different part numbers.
Second, the regional exposure shifts the jacket priority even when the movement duty is identical. A surface route in the Atacama needs UV performance sitting alongside abrasion resistance, which is where PUR earns its cost. An Indonesian nickel route puts water ingress and crush ahead of pure wear rate, because the cable spends its life in wet mud under machine traffic. Same duty class, different first question.
An approval in one jurisdiction is not an approval in another. A construction certified for Chinese coal mines is not thereby accepted under MSHA, and a cable built to AS/NZS is not automatically acceptable in the EU. Settle the acceptance route for your jurisdiction before the order is released rather than after it ships.
Route conditions that accelerate wear before you respec the cable
A jacket upgrade is sometimes the wrong fix. Several route conditions cause premature abrasion regardless of compound, and fixing them can extend service life more than swapping the material ever will.
- Unsupported drag length lets the cable find its own path across whatever surface happens to be sharpest, since nothing is guiding it.
- Sharp crossings and rib edges. One unprotected crossing point can wear through a jacket faster than kilometres of clean floor drag.
- Misaligned reel or level-wind — winding unevenly concentrates wear on one section of jacket instead of spreading it across the drum face.
- Cable left on the active floor gets crushed by passing shuttle cars, LHDs and supply vehicles, not just abraded (see the crushing note above).
- Wrong reel type for the duty. A compact spring reel built for light random winding, pushed past that duty, wears cable faster than any jacket upgrade can compensate for.
Crossing guards, roller supports, the right reel, and basic discipline about keeping cable off the active floor: all of that belongs in the same conversation as jacket selection, not tacked on afterward.
Reading a worn cable before you respec the replacement
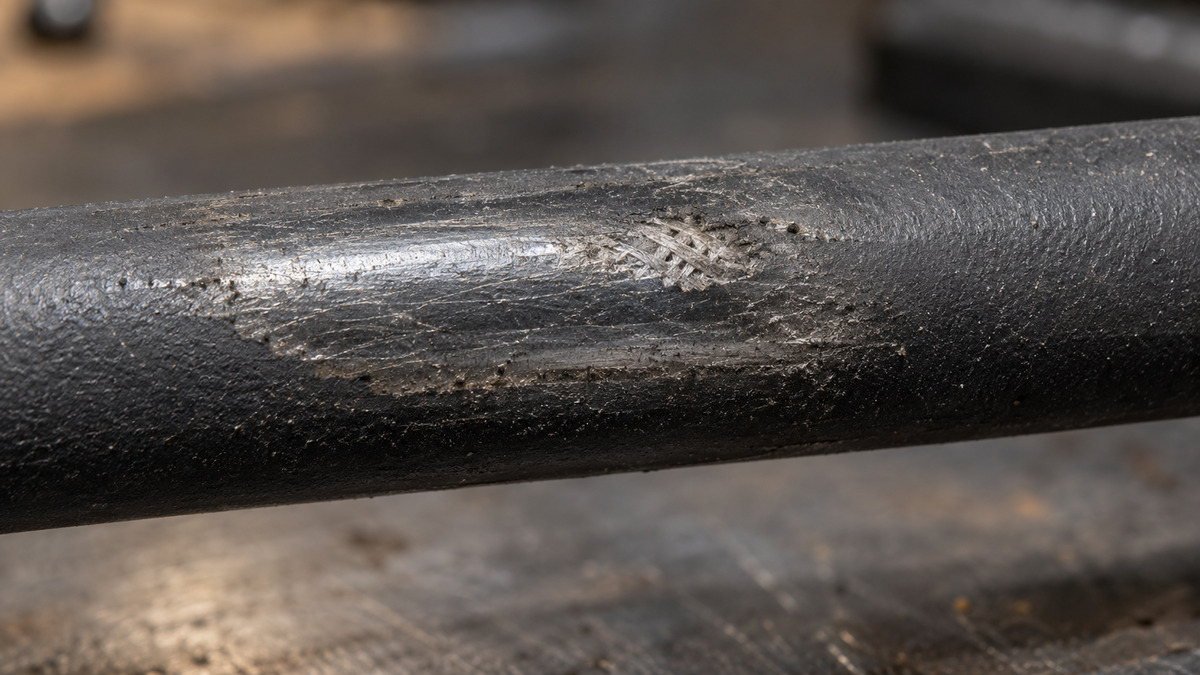
A failed cable is evidence. Read what happened to it before you order a like-for-like replacement.
| What you find | Likely cause | What to change |
|---|---|---|
| Even, gradual wear along most of the length | General drag abrasion against floor or rib | Confirm jacket compound and wall thickness are matched to the drag distance |
| A deep worn band at one point, rest of the cable intact | A single unprotected crossing or sharp edge | Fix the route point first; a jacket upgrade alone will wear through the same spot again |
| Flattened conductor, cracked insulation, jacket otherwise sound | Crushing under vehicle traffic | Change handling practice and routing, not the jacket compound |
| Wear concentrated near the reel or level-wind mechanism | Reel misalignment or wrong reel type for the duty | Check reel condition and rated duty before respeccing the cable |
See 0.6/1 kV mining cable selection for mobile equipment for the fuller failure-to-specification method this table is drawn from.
What the standards actually govern — and what they leave to the datasheet
The standards referenced on a mining cable datasheet mostly set mechanical and electrical construction requirements. Few mandate a specific abrasion test, so the compound and wall thickness need to be stated explicitly — a standard reference alone won’t cover it.
| Standard / regulation | What it governs | Abrasion coverage |
|---|---|---|
| ISO 4649 / DIN 53516 | Rotating-drum abrasion test method for vulcanised and thermoplastic rubber | Directly — this is the abrasion test itself |
| ICEA S-75-381 (North America) | Portable power cable construction: conductor, insulation and jacket thickness ranges | Sets mechanical thresholds but does not itself require an abrasion test |
| MSHA 30 CFR §18.35 | US portable (trailing) cable and cord construction for permissible face equipment: conductor sizing, jacket presence, flame acceptance | Specifies jacket construction requirements, not a named abrasion figure |
| MSHA 30 CFR §75.906 | Trailing cables for mobile equipment, ground wires and ground-check wires in US underground coal mines | Covers protection and grounding practice, not abrasion testing |
| AS/NZS 1802 / 2802 (Australia/NZ) | Coal and general mining cable constructions for trailing and reeling duty | Sets construction and mechanical requirements by application class |
Meeting a construction standard tells you the cable is built to accepted mechanical and electrical thresholds for its class. It says nothing about abrasion performance on its own, so put the jacket compound, wall thickness, and where it matters the test method and result, into the enquiry separately.
What we build in-house, and what we can document
An article that tells you to demand the compound, the wall thickness and the test method owes you a straight answer about its own position. Here is ours.
TEBAOFLEX has manufactured special cable in Taicang, Suzhou since 2014, on a site of more than 20,000 m² with roughly 15,000 m² of production and warehouse space. Twelve automated lines cover the sequence from rubber compounding through extrusion, braided screening, laying-up and packaging, and eight sets of high-precision test equipment cover the run from incoming material to finished cable. Annual capacity is around 150,000 km. Engineering runs to more than 30 people, ten of them with over fifteen years in cable, and the business holds more than twenty patents. Figures confirmed September 2026.
Why in-house compounding matters for this particular question. Rubber compounding runs on our own lines rather than arriving as a finished bought-in material, so the jacket recipe is something you can raise at specification stage instead of picking from a fixed menu. It also explains the processing row in the compound table above. A thermoset jacket such as CPE has to be cross-linked after extrusion, which is a real step in the production schedule; a thermoplastic TPU jacket does not. That difference shows up in lead time and in how a short custom run prices out, which is worth knowing before you ask for a compound change on a tight delivery.
Where we can hand you a certificate, and where we cannot. The clearest documentation we hold for mobile mining cable is the Chinese mine-safety (MA) set, which covers precisely the cable type this article is about: mobile shielded rubber-sheathed flexible cable for coal mines, including the monitored constructions that carry a pilot core.
| Construction | Standard | Certificate | Valid to |
|---|---|---|---|
| MYP 0.38/0.66 kV, 4–150 mm² | MT/T 818.5-2009 | MIA230337 | 22 March 2028 |
| MYP 0.66/1.14 kV, 10–150 mm² | MT/T 818.5-2009 | MIA230341 | 23 March 2028 |
| MYPT 1.9/3.3 kV, 35–150 mm² | MT/T 818.7-2009 | MIA230344 | 23 March 2028 |
| MYPTJ 3.6/6 kV, 25–150 mm² | MT/T 818.6-2009 | MIA230260 | 8 March 2028 |
| MYPTJ 6/10 kV, 25–150 mm² | MT/T 818.6-2009 | MIA230259 | 8 March 2028 |
| MYPTJ 8.7/10 kV, 25–150 mm² | MT/T 818.6-2009 | MIA230261 | 8 March 2028 |
Read that table literally, because its scope is narrow by design. Those certificates apply to Chinese coal mines, and only to the models and conductor cross-sections listed. They do not carry across to MSHA, AS/NZS or European acceptance. For those markets a construction is built to the named standard and the acceptance route is agreed for the project, which is a different statement from holding a mark. For European rubber flexible constructions we separately hold a VDE Marks approval, certificate 40060056, against DIN EN 50525-2-21.
On abrasion figures specifically: if your specification needs an ISO 4649 or DIN 53516 result for a particular compound at a particular wall thickness, ask for it explicitly with the enquiry, and ask what documentation can accompany the order. That number does not belong on a general catalogue page, and a supplier who quotes one without naming the method and the sample thickness has not given you anything you can hold them to. That test applies to us as much as to anyone else you are comparing.
Construction options for abrasion duty
TEBAOFLEX builds mobile-equipment mining cable across all three jacket families. Which one is right depends on the movement duty worked out earlier on this page, more than on the machine name.
| Construction | Jacket | Typical duty | Best fit |
|---|---|---|---|
| C800 extra-flexible PVC reeling cable | Transparent PVC | Compact spring reels, moving machine control and signal wiring | Confined installation envelopes with protected cable entry; the product’s own guidance points to a PUR reeling construction once abrasion exposure or random winding increases |
| GPM / GPM-RF PUR reeling cable | Abrasion-resistant polyurethane | Random-winding spring and motorised reels, monospiral storage reels, transfer equipment | Repeated winding duty and higher abrasion exposure than a compact PVC reel is built for |
| POLYFLEX MINE 0.6/1 kV PUR mining cable | UV-resistant polyurethane | Mobile power distribution on quarrying and open-cast plant, outdoor construction and industrial mobile installations | Combined abrasion and UV exposure on tracked or wheeled mobile plant working outdoors |
| SHD-GC 2–25 kV mining power cable | Extra-heavy-duty CPE, or project-specified TPU | Continuous miners, loaders, drills, jumbos, shovels and draglines | Heavy medium-voltage trailing duty, with a TPU jacket available where the project specifies it |
See the full range in mining, drilling and tunnelling cables, filterable by movement duty and voltage class. If the route you are specifying stays in one position rather than moving with equipment, see armoured mining cable instead: a fixed route carries a different construction priority than the mobile duty this page covers.
Common mistakes
- Comparing abrasion figures without matching test methods. A number from one datasheet means nothing next to a number from another unless both used the same test and sample thickness.
- Assuming the standard reference covers abrasion, when most construction standards only set mechanical thresholds. State the compound and thickness separately.
- Treating a crushed cable as an abrasion failure — the fix there is handling and routing, not a tougher jacket compound.
- Upgrading the jacket without fixing the route. A sharp, uncorrected crossing point wears through the next jacket too, whatever it’s made of.
- Picking a reeling cable by voltage alone, when the reel type, winding pattern and tension matter just as much — see the duty mapping above.
Information for an abrasion-duty cable enquiry
| Data group | Minimum information | Why it matters |
|---|---|---|
| Movement duty | Trailing, reeling, guided/festooned, or compact spring reel | Sets which surfaces and contact points cause wear |
| Route detail | Drag distance or reel type, crossing points, floor and rib condition | Route fixes can extend life more than a jacket change alone |
| Environment | Outdoor UV exposure, oil, water, chemical or temperature extremes present | Some jacket families combine abrasion resistance with UV or oil resistance better than others |
| Electrical | Voltage, current, screen and ground-check requirements | Sets the base construction the jacket is applied to |
| Failure history | Pattern of the cable being replaced (even wear, single point, crushing, reel-area wear) | Points to whether the fix is jacket compound, wall thickness or the route itself |
| Governing standard | Applicable regional standard and jurisdiction | Sets the mechanical and electrical construction baseline the jacket is added to |
Before specifying a custom jacket compound or thickness: confirm current lead time and minimum order quantity with our engineering team. As of August 2026, standard lead time runs 7–45 working days depending on product type, stock position and customisation, and the minimum order quantity is 50 m for both standard and custom constructions — both are subject to sales confirmation for your specific enquiry. A jacket compound change is a specification conversation, not a catalogue swap, so it is worth having early rather than at the point of order.
Questions buyers ask
What is the most abrasion-resistant jacket material for mining cable?
Thermoplastic polyurethane (TPU, often labelled PUR) generally outperforms CPE and PVC in published rotating-drum abrasion comparisons, but the result depends on the specific formulation, wall thickness and test method used. A material name alone does not guarantee an abrasion outcome — ask for the test data behind it.
Is polyurethane always better than CPE for mining cable jackets?
Generally yes on abrasion and tear resistance, but that’s not the whole story. CPE remains a proven, widely specified mining jacket with good cold flexibility and years of track record behind it. The right choice depends on the movement duty, temperature range, flame requirements and cost target for that specific route.
How is cable jacket abrasion resistance tested?
The common method is a rotating-drum abrasion test — ISO 4649 internationally, or the related DIN 53516 method — in which a sample is rubbed against a standard abrasive sheet and the material lost is measured as a volume. A lower volume loss means better abrasion resistance, but figures are only comparable when the test method and sample thickness match.
Does a thicker jacket automatically mean better abrasion resistance?
A thicker jacket has more material to wear through, which extends life against gradual abrasion, but it doesn’t change the compound’s underlying wear rate. Added thickness also increases stiffness and weight, which can work against flex life on a trailing route. Size thickness and compound together rather than trading one off against the other.
Should I choose a jacket based on abrasion resistance alone?
No. Abrasion resistance has to be weighed against flexing life, cold-temperature performance, flame and smoke behaviour, and cost for the specific duty. A jacket optimised only for abrasion can be the wrong choice if it sacrifices flexibility a trailing route needs, or cold performance a surface route needs.
Source and review status
Test-method and standards descriptions reflect published ISO, DIN, ICEA, MSHA and AS/NZS documentation as referenced above. Jacket-material comparisons reflect published manufacturer technical literature, cited where a specific figure is used. Construction and application details for TEBAOFLEX products reflect the current product pages linked on this page. Manufacturing, capacity and personnel figures are internal records confirmed September 2026; certificate numbers, scopes and expiry dates were verified against the certificates on 17 August 2026 and should be re-confirmed at enquiry. Regional supply patterns reflect our own export experience; the characterisation of what dominates jacket exposure in each region is engineering judgement applied to those conditions rather than measured field data, and site-specific conditions should always be verified. Reviewed 7 September 2026.
Send the duty, not just the cable type
State the movement duty, route conditions and failure history of the cable you are replacing — photographs of the worn section are more useful than a part number. Our engineering team will use them as the starting point for a jacket and construction review. Remote technical review by video call, meeting or email is free; a cross-border site survey is quoted separately on request.